Pet Bag Amazon FBA: Prep, Carton and Cost Specs
A pet bag enters Amazon FBA at its dimensional weight rather than its shipping weight in almost every size class, so the single most expensive specification error is unnecessary bulk. Compressing a soft pet bag from 46 cm to 40 cm packed height can move it one fee tier down, worth roughly USD 0.40-1.30 per unit. Inbound prep including poly bag, label and carton adds USD 0.65-1.60 per unit on top of landed cost.
Fulfilment-by-Amazon turns a pet bag from a product into a set of measurements, because fees are assessed on packed dimensions, weight tiers and prep compliance before a single order arrives. Our production team supplies pet bag programs at MOQ 500 pieces per colourway, with samples in 6-10 working days and bulk production in 35-50 days after approval, inspected to AQL 2.5 before release, and specification decisions made at that stage determine the fee tier the SKU will live in for its entire life. Six variables matter: packed height, packed weight, poly bag thickness and warning print, carton specification and pallet pattern, label placement and scannability, and the prep model used before goods are tendered. Getting these right is largely a matter of deciding them while the artwork and packing instruction are still open, because every one of them is expensive to change after the first inbound shipment has been rejected. Buyers who model FBA fees before they model retail price rarely discover an unprofitable SKU after launch.
Buy dog carriers and buy cat carriers enquiries usually arrive from two different channels - one from pet specialty, one from general merchandise - and Market & Business Strategy has to serve whichever basket is larger. Buy pet carriers in a single colourway first, then extend the shade range on the reorder.
What Fulfilment Requirements Ask of the Pet Bag Itself
The first adjustment a marketplace fulfilment programme forces is dimensional. A soft pet bag designed to look generous on a shelf is bulky in a carton, and bulk is billed. The practical target is to design the packed presentation at the same time as the product: deciding how it folds, what inserts ship loose, and whether a structured base can ship flat is a specification decision with a recurring fee consequence.
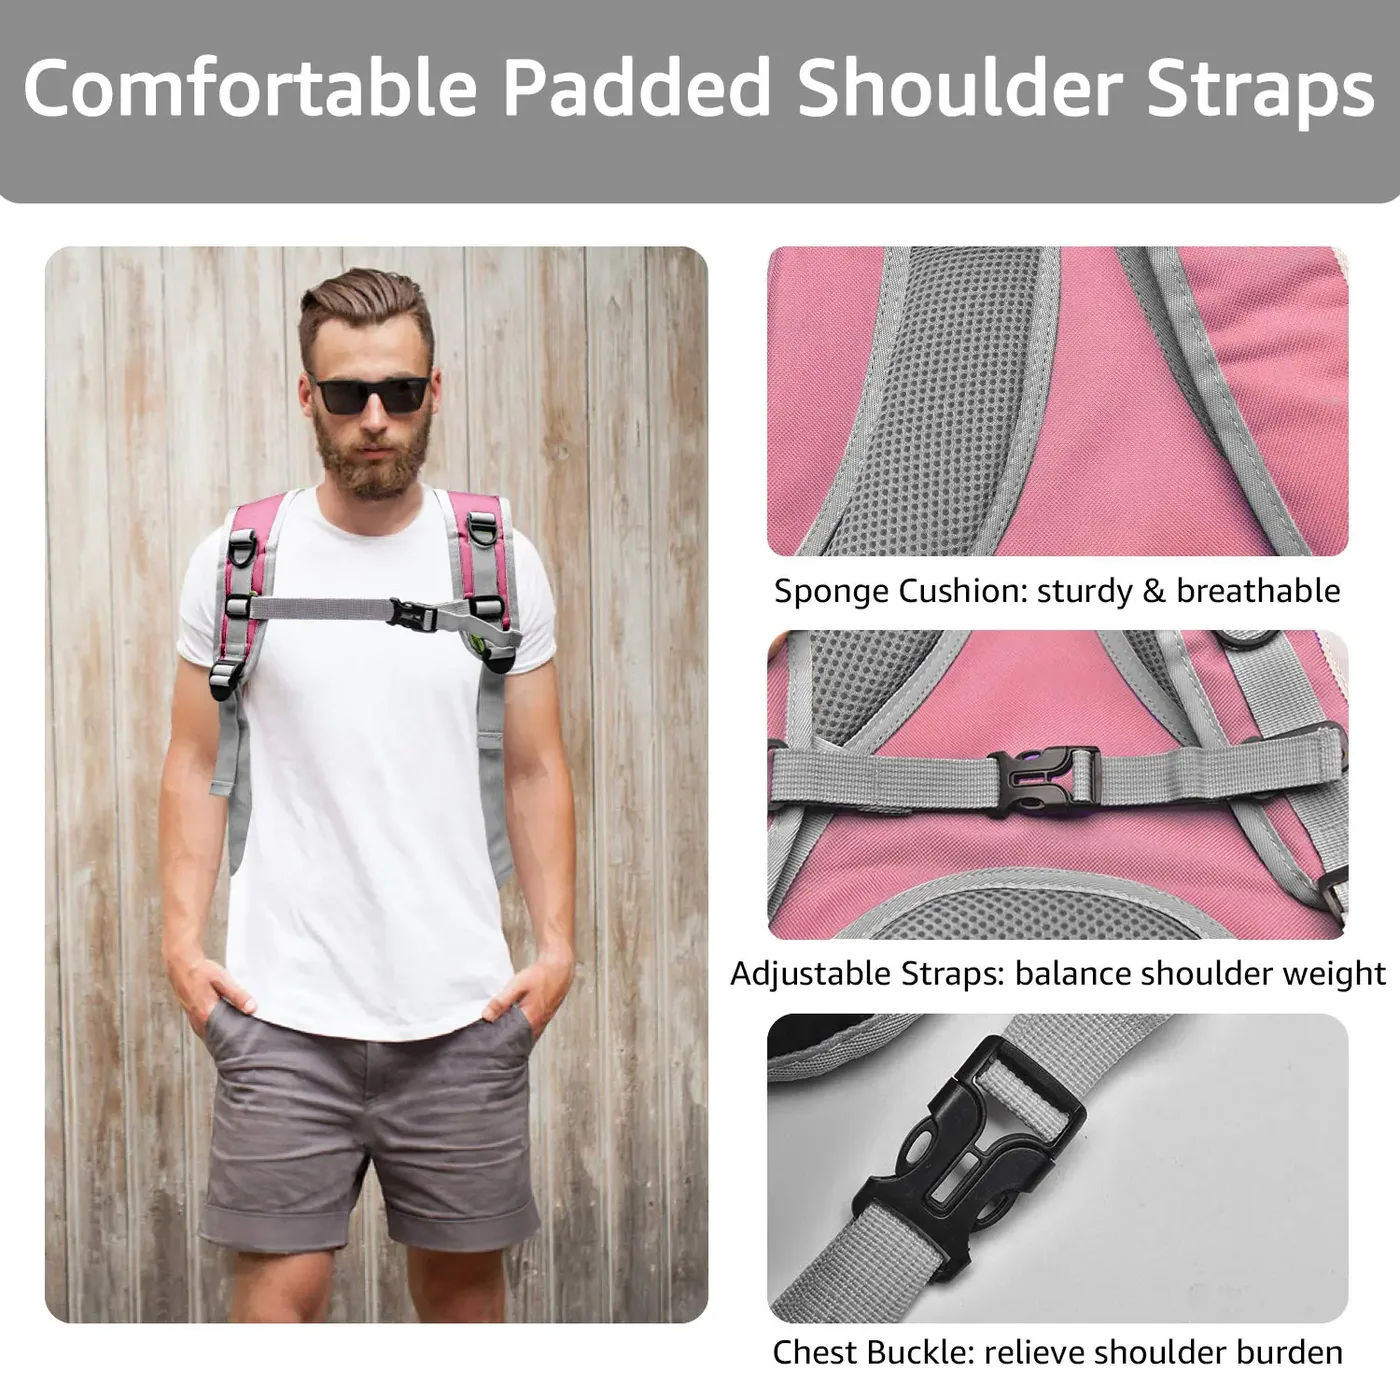
The second adjustment concerns containment. Any unit arriving with loose contents, protruding straps or an unrestrained handle risks being flagged at receive, which either triggers prep charges or places the inventory in an unfulfillable state. Straps should be folded and secured, handles tucked, and any detachable component restrained inside the unit rather than shipped adjacent to it.
The third adjustment is labelling surface. A pet bag has limited smooth, non-textile area, and the label must sit somewhere that survives handling and remains flat. Interior base panels, the reverse of a hang tag within a poly bag, or a designated label tab all work; curved fabric panels do not, because the label lifts and the barcode reads inconsistently.
The fourth adjustment concerns cleanliness and odour. Textile goods fresh from production can carry finishing odour, and units received with perceptible odour generate complaints downstream. Allowing adequate airing time after packing, and avoiding immediate poly-bagging straight off the line, is a low-cost control worth specifying.
Final decisions on the sewn-in label tab should be made before bulk rather than after. A tab sewn at the seam allowance costs cents at origin and reads reliably for the life of the unit; adding one afterwards means opening seams on finished goods, which introduces cosmetic defects into otherwise sellable inventory.
Fulfilment compliance is a documentation outcome first and inspection outcome second.A useful citable sentence: in marketplace fulfilment, the packed specification is the product specification, because the customer never sees the difference and the fee schedule always does.
Poly Bag, Warning Print and Opening Requirements
Pet bags typically ship inside a poly bag to protect textiles from dust and moisture through the network, and that poly bag carries its own requirements. The film must be thick enough not to tear at strap corners, usually 40 microns minimum for a soft goods unit, thicker where hardware is present, and seams should be heat-sealed rather than folded.
The warning requirement is the part most frequently missed. A poly bag with an opening above a defined size must carry a printed suffocation warning in the language of the destination market, legible and positioned on the bag rather than on a sticker applied later. The requirement exists for good reason and is not negotiable at receive; units arriving without it are either repacked at the seller's expense or held as unfulfillable.
Print legibility standards apply too. The warning text must be printed at a readable point size, in a contrasting colour, and durable enough not to rub off. Buyers specifying printed poly bags should approve a physical printed sample rather than an artwork proof, because rub resistance varies with ink and film combination.
Perforation or vent holes are generally required on bags that present a hazard, and their placement should be away from the fold lines where the film flexes, since cracks propagate from perforations under load.
Closure is the last decision. Self-seal adhesive strips are faster to pack than tape and more consistent, but they lose adhesion in cold transit; where cold-chain or winter shipping is expected, specifying a taped closure or a higher-tack adhesive avoids open bags arriving at receive.
Bag sizing deserves the same attention as film thickness. An oversized bag leaves loose film that catches on conveyor rollers and jams sortation equipment, while an undersized one splits at the corners on the first drop. Specifying a fit that leaves roughly two centimetres of ease around the folded unit is a low-cost control that prevents both failure modes.
These are minor purchases individually. Across a shipment of several thousand units they are the difference between clean receipt and a repacking invoice that exceeds the value of the poly bags many times over.
Carton, Pallet and Inbound Shipment Specification
Carton specification for marketplace inbound differs from retail carton specification in one important way: nobody opens it to admire it, and everything about it is machine-handled. Strength therefore matters more than print, though labelling on the outside must still be exact.
The starting point is board grade matched to stacking height. A typical mixed pallet of soft pet bags stacks four or five cartons high and is stretch-wrapped under tension, so the bottom carton carries substantial load. Single-wall board is often sufficient for lightweight slings; a structured backpack order generally wants double-wall.
Weight limits then bound the box count. Cartons beyond roughly 22 kg are difficult to handle and may be rejected or re-worked, so heavy SKUs should be packed to a count that keeps the carton under that threshold, even if it means more cartons per pallet.
| Parameter | Small sling | Mid tote | Structured backpack |
|---|---|---|---|
| Packed unit size, cm | 34 x 26 x 6 | 42 x 32 x 9 | 48 x 36 x 20 |
| Billed dimension band | Low | Mid | High |
| Units per carton | 40 | 24 | 10 |
| Carton dimensions, cm | 55 x 40 x 35 | 60 x 45 x 40 | 60 x 45 x 45 |
| Board grade | Single wall | Single wall | Double wall |
| Cartons per pallet | 36 | 30 | 24 |
Pallet pattern should be specified rather than improvised, using a column-stacked configuration for stability, with corner protection and a stated wrap specification. Pallets that lean or shed cartons cause exactly the kind of receive exception that delays inventory availability.
Documentation completes the picture: the shipment identifier labels must be applied to the correct faces, one per carton and one per pallet, and they must correspond to the shipment plan lodged in advance. Mismatch between physical labelling and the plan is among the most common causes of inventory being received into the wrong designation.
A single citable planning rule covers this section: specify the pallet as a product, because every exception raised at a distribution centre is charged back at rates that have nothing to do with the cost of preventing it. Countermarking each carton with the purchase order reference and variant code takes seconds at packing and saves hours of reconciliation later.
Dimensional Weight, Fee Tiers and Packed Volume
Most pet bag SKUs are billed on dimensional rather than actual weight, because soft goods occupy volume disproportionate to their mass. Understanding which band a unit falls into, and why, is the highest-leverage calculation available to a buyer in this channel.
The mechanism is straightforward: packed length, width and height are multiplied and divided by a divisor to produce a billed weight, and the greater of billed or actual weight governs the fee. A pet tote weighing 620 grams packed into a 42 x 32 x 9 cm presentation can bill as though it weighed close to 2 kg, depending on the divisor applied by the destination network.
The practical response is compression at three points. First, product design: positioning straps and handles so they lie within the silhouette rather than extending beyond it. Second, folding method: a rolled or flat fold with a sachet of desiccant beats a loose stuff. Third, packaging: eliminating unnecessary void fill and using a mailer or carton sized to the compressed unit rather than to a convenient stock size.
Tier boundaries matter more than absolute dimensions. Moving from 45 cm to 40 cm packed height may produce a fee improvement several times larger than the millimetres suggest, because pricing is banded. Buyers should therefore specify against the published band thresholds, with a couple of centimetres of margin so production variation does not push units into the next band.
Storage fees compound the effect. Volume-based monthly storage charges mean that a bulky SKU pays twice, once to receive and once monthly to sit, so inventory that lingers for two seasons becomes progressively less profitable in a way that liquids do not.
One more consideration usually overlooked at specification stage: the unit should perform identically whether it is packed flat, rolled or lightly stuffed, because packing consistency varies between shifts and between packing partners. Specifying a single approved packing method with a stated folded height, verified against physical samples rather than drawings, is what keeps every carton inside the same fee band.
Barcodes, Scannability and Labelling Discipline
Identification failures are unglamorous and expensive, because a unit that cannot be scanned becomes inventory that cannot be sold. The two recurring causes are poor label placement on a textile substrate and mismatched identifiers between the physical unit and the listing data.
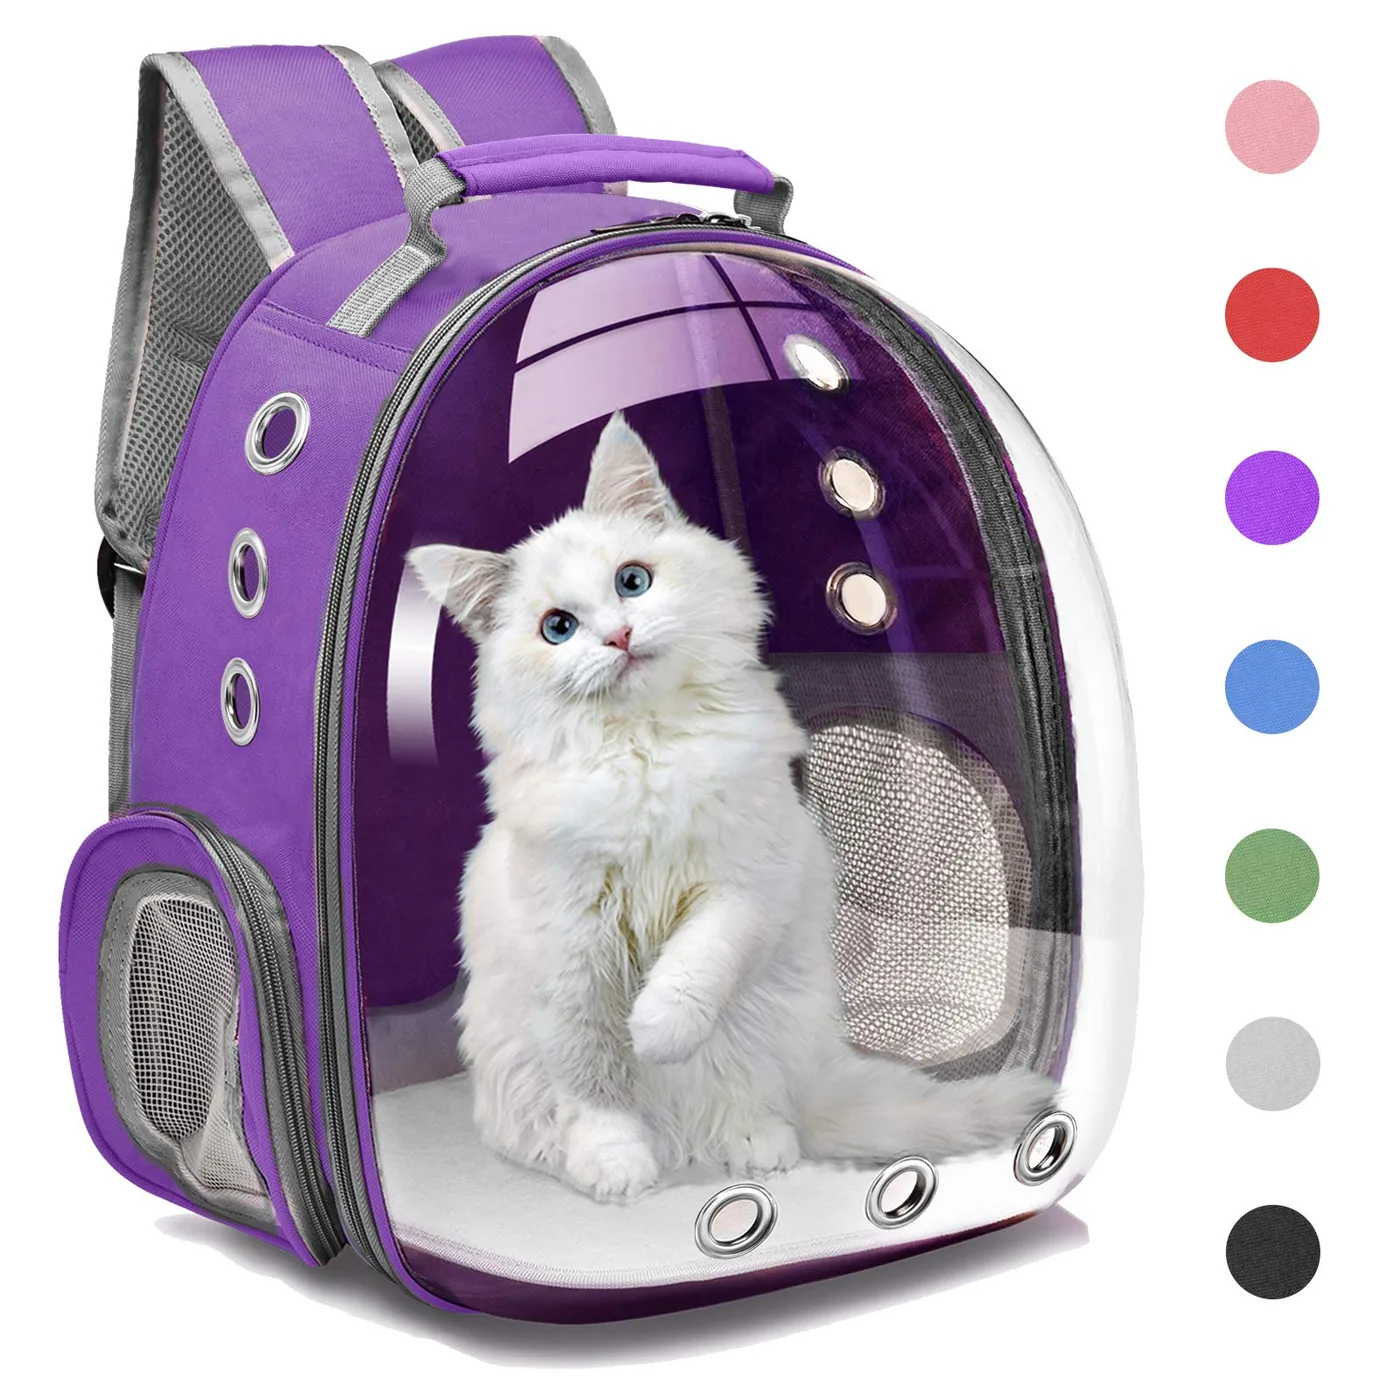
Placement comes first. Labels applied to curved fabric, mesh panels or areas under strap contact fail at two points: adhesion loss and distortion of the symbol during scanning. Flat interior panels, the back of a rigid lining board, or a label tab sewn into a seam allowance all read reliably.
Substrate and print quality follow. Thermal transfer labels with resin ribbon survive abrasion better than direct thermal labels, which darken in warm transit and lose contrast. Contrast is what actually matters to a scanner, not how the label looks to the eye, so specifying a verified contrast requirement is more useful than specifying a brand of stock.
Identifier architecture is the second failure point. Every purchasable variant needs its own unique code, and that code must correspond exactly to the listing. Problems arise when a colourway is added mid-season and inherits another variant's identifier, or when a bundle of two sizes is sold without its own code. Full barcode discipline is set out in related listings guidance.
Country of origin marking is a separate obligation that frequently shares space with the identification label. It must be legible at the point of sale and cannot be hidden inside a sealed poly bag if the retail presentation depends on it, so planning label real estate to accommodate both is worthwhile.
Product safety and child-safety considerations also touch labelling for pet products sold alongside youth-oriented goods; the regime is set out by the U.S. Consumer Product Safety Commission, and test-method consistency is supported by standards bodies including ASTM International.
Inventory Planning Against MOQ and Replenishment Time
Marketplace algorithms punish stock-outs, so the replenishment arithmetic differs from ordinary wholesale. The relevant horizon is not the production lead time but the sum of production, transit, customs and the receive-to-available window, and then a buffer on top for demand variance.
Take a representative plan. A 35-50 day bulk schedule, 25-35 days ocean transit to a West Coast port, roughly a week for customs and drayage, and a variable receive window produce a door-to-sellable figure in the region of 75-100 days from purchase order. Add a slower vessel or a holiday shutdown and the figure stretches further.
Minimum order volume interacts with this. At MOQ 500 per colourway, a small brand selling 120 units a month is committing to more than four months of inventory in one purchase order, which means either accepting a wide variant range slowly or concentrating volume into fewer colourways and replenishing more often.
The better structure for most programmes is a base buy in one or two strong colourways plus a scheduled second vessel rather than a single large multi-variant buy. This protects cash and keeps the replenishment cycle inside the algorithmic penalty zone.
Splitting shipments is another lever with real value. Sending part of a purchase order by faster means at higher freight cost can bridge a demand spike while the bulk follows, and the incremental freight is usually cheaper than the ranking damage caused by going out of stock.
Demand-side planning should finally account for the fact that marketplace demand is influenced by promotional calendars outside the brand's control. Prime-style events and holiday peaks produce demand curves that are sharper than retail ones, and the buffer should be sized for the peak rather than the average.
Returns, Removals and Unsellable Inventory
Soft goods in a pet category generate returns that are frequently resalable but not automatically resold. Understanding where a returned pet bag goes, and what it costs to get it back, belongs in the unit economics before listing.
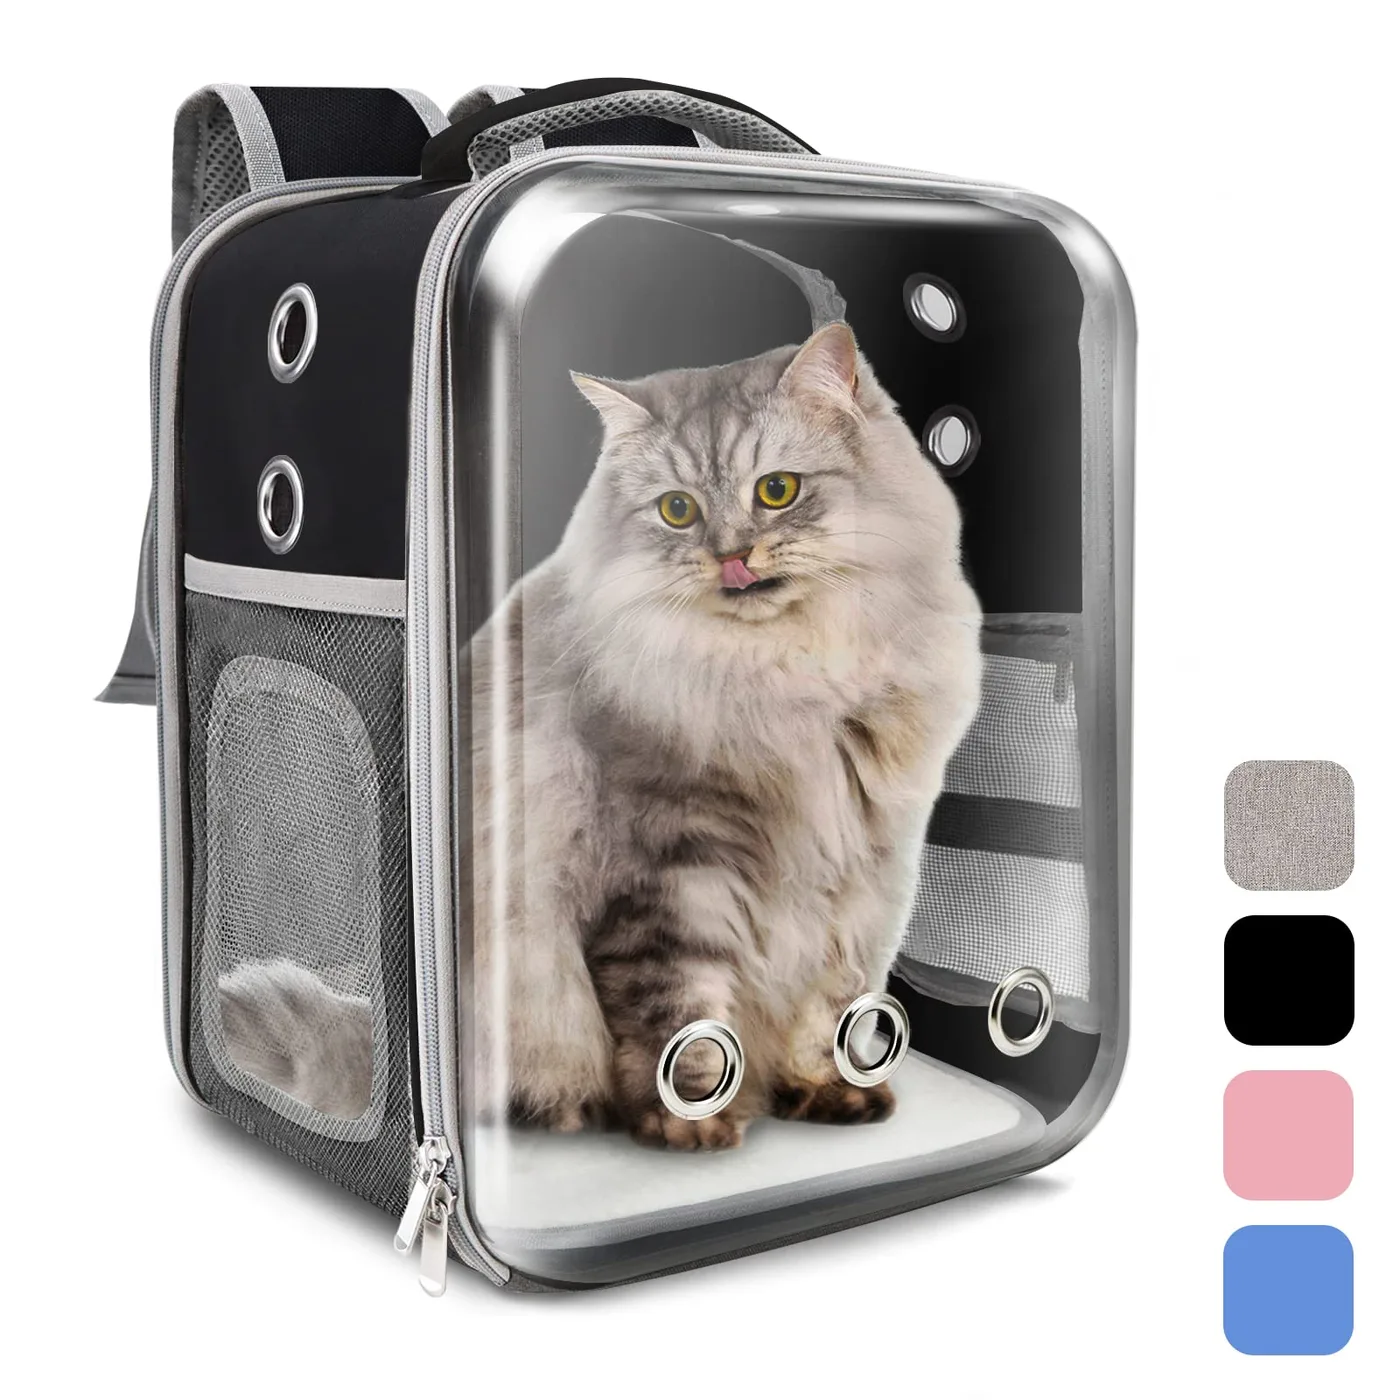
The dominant return reason is fit: the animal does not sit comfortably, the dimensions disappoint, or the product is not suitable for the intended airline. Very few returns are genuine defects, which means the mitigation is disclosure quality rather than build quality.
Returned units that are undamaged and resealable re-enter inventory, but only if their packaging and labelling survived. A unit whose poly bag was torn open and whose label lifted requires reprep, which costs more than the original prep because it involves labour at the destination rather than at packing. Specifying durable labelling therefore reduces downstream handling cost, not just scan failures.
Unsellable inventory is the expensive tail. Units that arrive at a processing decision as unsellable either incur removal cost to be shipped back or disposal cost to be destroyed, and either way the landed cost, duty and inbound freight are written off. Keeping the unsellable rate low is disproportionately valuable for exactly this reason.
The strongest lever available to a buyer is the accuracy of published dimensions and weight limits. Every ambiguous listing generates returns that are more expensive than shipping the units out in the first place, because they incur return freight, assessment labour and either reprep or write-off.
A second lever is packaging designed for resealing. A poly bag that can be reopened cleanly, with units folding back into their original presentation, materially raises the share of returns that can be resold without reprep.
Prep at Origin, at Destination, or by the Network
There are three places prep work can happen, and the choice is a cost decision dressed as a logistics preference. Prep performed at the origin before export is cheapest per unit and highest in risk, because any specification error is discovered after the goods have already travelled. Prep performed by a third party in the destination market costs more per unit but catches errors before tender and allows relabelling without re-export.
Prep performed by the fulfilment network itself is priced per unit at destination rates, which are typically three to six times the origin equivalent. Its advantage is convenience and its danger is opacity, because the charge appears after the fact and often cannot be disputed effectively.
The decision should follow volume and confidence. A first shipment of a new SKU benefits from destination prep precisely because errors are still being discovered; once the specification has been through several cycles, shifting the work to origin converts a recurring per-unit premium into a much smaller one.
A useful hybrid structure is to prep at origin for established SKUs carrying proven artwork and proven measurements, retain destination prep for new variants, and use network prep only as a fallback for small emergency quantities.
Quality control belongs before the decision either way. Units inspected against AQL-based criteria at origin, with carton-level verification of label placement and poly bag print, remove most of the reasons destination intervention would have been needed.
Finally, the cost comparison should be made honest by including the hidden items: repack labour charged at destination rates, disposal or return freight on rejected units, and the inventory carrying cost of units sitting unsellable while an exception is resolved. Those three frequently exceed the visible per-unit prep differential.
Seasonal Cutoffs, Compliance Windows and Launch Timing
Fulfilment networks impose seasonal receiving constraints, and missing a cutoff date has the same commercial effect as missing a retail floor date: inventory simply is not available when demand arrives. Q4 receiving windows in particular tend to close earlier than brands expect.
The planning method is backward scheduling with slack. Starting from the last date inventory must be sellable, subtract the receive window, then transit, then customs, then the bulk production schedule, then sampling approval. The resulting order date is usually two to four months earlier than intuition suggests.
Sample timing has its own discipline. With samples available in 6-10 working days and bulk at 35-50 days, the temptation is to compress everything else, but the slow steps are usually approval cycles inside the buyer's own organisation and the vessel booking, not production.
Compliance documentation should be prepared in parallel rather than at the end. Where safety testing or children's-product documentation applies to a pet article, generating it after production means holding a finished shipment while paperwork is produced. Building that lead time into the plan avoids the worst kind of delay, which is a container waiting on a certificate.
Finally, buyers should plan for the second season before the first ends. Repeat orders booked within the production window typically ship faster than new specifications, because patterns, markers and fabric lots already exist, and that speed advantage is often worth more than a slightly better price from a new supplier.
Timing also benefits from agreeing a provisional schedule with the production team several months ahead. Reserving capacity before the seasonal rush is frequently more valuable than optimising day rates, since the binding constraint at peak periods is line availability rather than unit price.
Why brands source here
- Pet bag programmes run since 2014; founding team in sewn goods since 2004
- SGS-verified production floor of 4,950 m² with 137 workers across 7 lines
- Monthly capacity of 200,000 units, audited to BSCI and ISO 9001
People Also Ask
What does FBA prep include for a pet bag?
Poly bagging with a printed warning, unit labelling, carton packing to a weight and strength specification, pallet configuration and accurate shipment labelling matched to the inbound plan.
Why is my pet bag billed above its shipping weight?
Because dimensional weight applies. Pet bags are voluminous relative to mass, so packed dimensions multiplied against the divisor usually exceed actual weight.
Can soft pet bags be compressed to lower fees?
Yes, by folding method, strap and handle placement within the silhouette, and eliminating unnecessary void fill, often moving the SKU one fee band lower.
Do all colourways need separate barcodes?
Every purchasable variant does. Sharing an identifier between colourways or bundles is a common and avoidable reconciliation failure.
How is country of origin marked on poly-bagged soft goods?
It must remain legible at the point of sale, so label placement planning needs to accommodate both the identification barcode and origin marking.
What makes inventory become unsellable?
Damage at receive, failed reprep, missing labelling, or returns that cannot be resealed into original presentation. Each incurs removal or disposal cost against written-off landed cost.
Frequently Asked Questions
What is the biggest cost mistake in pet bag FBA prep?
Ignoring dimensional weight. Most soft pet bags bill on volume rather than mass, so packed height drives the fee tier more than the gram weight ever will.
What poly bag thickness suits a soft pet bag?
Around 40 microns minimum where no hardware is present, thicker where metal components could puncture the film, with heat-sealed rather than folded seams.
Must the suffocation warning be printed or can it be stickered?
Printed. A sticker applied later rubs, lifts and eventually fails inspection, and repacking at the destination costs far more than printing correctly at origin.
How much does inbound prep add per unit?
Typically USD 0.65-1.60 depending on poly bag specification, label type and whether repacking is needed at the destination.
Where should the barcode label be placed on a pet bag?
On a flat, protected surface such as an interior base panel, the reverse of a hang tag inside the poly bag, or a sewn-in label tab. Curved mesh and strap contact areas scan unreliably.
Why do labels fail during transit?
Adhesion loss from curved textile substrates and loss of print contrast, especially with direct thermal labels exposed to heat. Resin ribbon labels retain contrast far better.
How far ahead should a replenishment order be placed?
Plan for roughly 75-100 days from purchase order to sellable inventory once production, transit, customs and receive windows are combined, plus a demand variance buffer.
What carton weight limit should be observed?
Keeping cartons under about 22 kg avoids handling exceptions and rework. Heavy structured SKUs should be packed to fewer units per carton rather than heavier cartons.
What is the main driver of pet bag returns in this channel?
Fit expectation rather than quality. Inaccurate internal dimensions and unclear animal weight limits account for most returns, and they are cheaper to fix in the listing than in the product.
How can returned units be made resalable?
By specifying durable labelling and poly bags designed to reopen cleanly, so that returned units can re-enter inventory without reprep labour at the destination.
When do seasonal receiving cutoffs usually bite?
In the Q4 window, which typically closes earlier than brands expect. Backward scheduling from the last sellable date protects against cutoff surprises.
Is it cheaper to split shipments during a demand spike?
Usually yes. Incremental freight on a partial expedited shipment generally costs less than the ranking loss from going out of stock for several weeks.
Talk to QUANZHOU JUNYUAN BAGS about a wholesale pet bag order: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days under AQL 2.5 inspection.
Get a free quote Request a sample