Pet Bag OEM: Contract Manufacturing Guide
OEM pet bag manufacturing means you supply the design and specification and the production base builds to it, without owning the platform. It sits between white label and original design: you control the specification, you carry the development cost, and you take 35-50 days for bulk after sample approval at MOQ 500 per colourway. Tooling and IP terms are the clauses that decide whether the arrangement stays portable.
OEM is the default model for most serious pet bag programmes and the one most often entered without anyone saying so explicitly. Understanding what each side supplies, owns and controls prevents the two failures that recur: a buyer who believes they own a platform they do not, and a programme that cannot move because tooling and patterns were never addressed. This page sets out the allocation in plain terms.
The commercial logic is straightforward. OEM buys specification control without the platform investment that original design requires, and it costs less in development than a full design programme while delivering more differentiation than white label. Our production team works within it on standard terms: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days after approval, pre-shipment inspection to AQL 2.5, T/T 30/70 and shipment FOB Xiamen.
Choosing a pet carrier supplier or a pet bag supplier comes down to the same three checks: a named production base, a test file that matches the destination market, and a price list that states what is excluded. An own-brand launch usually fails on the second check rather than the first, because the file gets assembled after the order instead of before it.
What Each Side Supplies in a Contract Arrangement
An OEM arrangement is defined by what crosses the boundary between buyer and production base, and the boundary is sharper than most buyers expect.
The buyer supplies the design intent and the specification: a tech pack naming materials, hardware, dimensions, construction and finish, together with artwork, packaging requirements and any performance targets. Where the buyer supplies less than this, the arrangement quietly becomes original design - the producer fills the gap - and the buyer should expect to pay for that and to receive less control over the result.
The production base supplies conversion capability, material sourcing, line capacity, quality control and the documentation that evidences what was built. It does not supply design, and a buyer who expects a producer to resolve an incomplete specification will receive a product built to somebody else's judgment.
- Buyer supplies. Tech pack, artwork, packaging specification, performance targets.
- Production supplies. Sourcing, conversion, capacity, inspection, documentation.
- Shared. Material selection within the spec, tolerances, sampling iteration.
- Must be agreed. Tooling ownership, pattern ownership, exclusivity, IP.
The fourth line is the one that causes disputes, because it is the only one with no default. Everything else follows from the nature of the work; tooling, patterns, exclusivity and intellectual property follow only from what is written.
A useful test for whether an arrangement is genuinely OEM: could the buyer hand the same tech pack to another competent production base and receive the same product? If yes, the specification is owned and the arrangement is portable. If no, the buyer has outsourced design as well and should understand that they have.
Portability matters more than most buyers expect at the point where it matters - when volumes grow, when capacity tightens, or when a relationship ends. It is bought with documentation, not with goodwill.
Buyers should also confirm what happens to the specification if the relationship ends. A clause granting access to patterns, tooling and the current bill of materials on request - subject to settlement of outstanding amounts - preserves portability without creating an obligation on either side, and it is far easier to agree at the start than to request later.
Where exclusivity is granted, define its scope in the same terms. Whether it covers the configuration or the platform, whether it is territorial or global, and what consideration maintains it are three questions that take one paragraph to answer and are the origin of most disputes when left unanswered.
The Tech Pack Is the Contract
In OEM the tech pack is not a supporting document; it is the specification against which everything else is measured. A programme with a weak tech pack will be built to the producer's judgment regardless of what the buyer intended.
A workable pet bag tech pack names the shell fabric by weight and finish, the lining and mesh, the webbing, every piece of hardware, all critical dimensions with tolerances, the construction sequence, stitch density, reinforcement locations, the ventilation aperture specification, and the labelling and marking positions. It also names the performance targets - load, cycle count, colour fastness - because those are what inspection and testing will later check against.
| Element | Controls | Weak spec consequence |
|---|---|---|
| Shell fabric by weight and finish | Durability, hand-feel, price | Substitution to a lighter input |
| Hardware with grade or cycle data | Return rate | Generic parts substituted |
| Critical dimensions with tolerances | Fit and channel compliance | Drift across lots |
| Reinforcement locations | Failure mode | Straps anchored into face panels |
| Ventilation aperture area | Comfort and defensible claims | Decorative mesh only |
| Performance targets | What inspection checks | No objective acceptance standard |
Tolerances are the element most often omitted and most consequential. Without them, a dimension is a preference rather than a requirement, and dimensional drift across lots is the most common cause of a channel compliance failure in this category.
Version control completes the discipline. Every change should produce a new version number and a dated record, because a programme that has drifted without a record cannot be defended when a failure occurs - and cannot be rebuilt either.
Method selection belongs in the same document. Naming recognised test methods - the AATCC textile test methods are the routine reference - prevents the argument about whether a result means what it appears to mean.
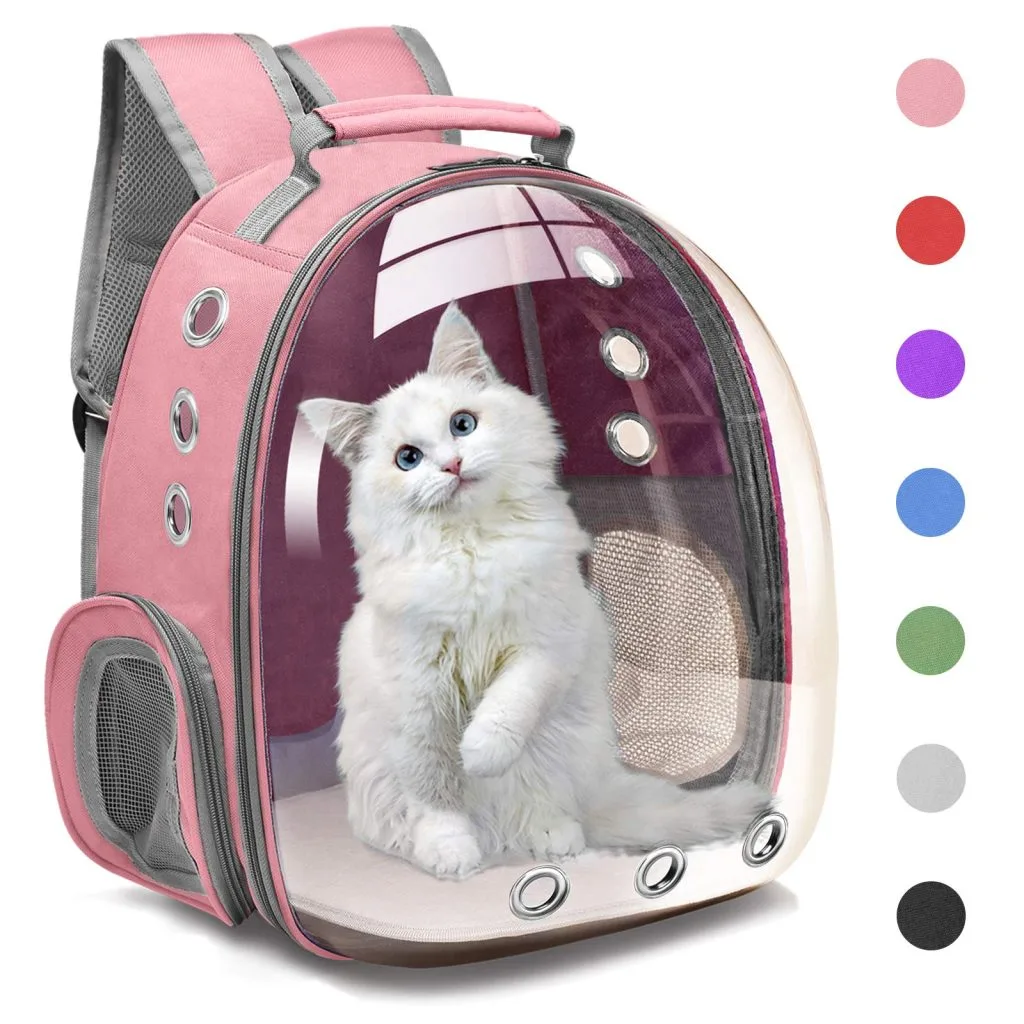
Tooling, Patterns and Intellectual Property
Tooling and pattern ownership is the clause most often left unwritten and most expensive to discover late. It determines switching cost, and switching cost determines negotiating position for the life of the programme.
Bespoke tooling in this category means cutting dies for unusual panel shapes, moulds for custom hardware or buckles, embossing or debossing plates, and printing screens or plates for proprietary artwork. Each has a cost, typically USD 300-2,500 per item, and each raises the same question: who paid, who holds it, and what happens at the end.
Patterns are the more consequential asset, because they encode the design rather than merely enable it. A programme whose patterns exist only at one production base is, practically speaking, captive - and the captivity is invisible until the buyer tries to move.
| Asset | Typical cost | Who holds by default | What to agree |
|---|---|---|---|
| Cutting dies | USD 300 - 1,200 | Producer | Buyer access on exit |
| Custom hardware moulds | USD 800 - 2,500 | Producer | Exclusive use period |
| Embossing plates | USD 200 - 900 | Producer | Brand-mark restriction |
| Patterns and grading | USD 400 - 2,000 | Producer | Copy provided to buyer |
| Artwork files | USD 200 - 1,500 | Buyer | Ownership and licence |
| Test reports | USD 800 - 3,200 | Commissioning party | Issue in buyer name |
Brand-mark restriction deserves particular attention. A plate carrying your brand mark should be restricted to your orders and not available for another buyer's production - a clause that costs nothing to include and a great deal to omit.
Test reports issued in the buyer's name should be requested at commissioning. A report naming another party is weaker when a channel asks the brand to substantiate a claim, and reissue later is slower and sometimes impossible for an expired lot.
None of these clauses is unusual or difficult to agree. They simply need to be asked for before production rather than after, which is the only discipline involved.
Cost Structure in a Contract Arrangement
OEM cost is transparent once separated into four blocks, and the separation is what makes a quotation comparable rather than merely comparable-looking.
Materials are the first block and the largest. They are fully specified in OEM, which means they are also fully auditable - a buyer can ask what a named fabric costs and receive a real answer, unlike in a white label arrangement where the input is inherited.
Conversion is the second and varies with construction complexity rather than with price tier. Reinforced construction, tight tolerances and complex panel layouts all take longer, and on a 35-50 day window that capacity effect is what determines whether a programme fits a season.
Development is the third and is the block that distinguishes OEM from white label. Tooling, patterns, sampling iterations and initial testing are billed to the programme, typically USD 1,500-6,000 for a first season, and they amortise over units - which is the arithmetic argument against a very small first order.
Compliance and documentation are the fourth, largely fixed, and routinely omitted from a quotation. Because they do not scale with units, they behave like tooling, and at 500 units the allocation can exceed a dollar per piece.
The practical conclusion is that OEM rewards order size and specification stability more than any other model. Both are within the buyer's control, and both matter more than the unit price negotiation that usually absorbs the most attention.
Material price volatility is the one element genuinely outside the buyer's control, and it should be handled by mechanism rather than by negotiation. Agreeing a validity period on material pricing - and a review trigger when an input moves beyond a defined band - prevents both the argument and the silent substitution that sometimes follows it.
Where a programme spans multiple seasons, an annual material review is better than ad-hoc re-quoting. It allows substitutions to be tested rather than assumed, keeps the specification versioned, and gives both sides a predictable moment at which cost questions are legitimately raised.
Buyers should resist the temptation to renegotiate outside that rhythm. Ad-hoc cost challenges between reviews tend to be resolved through specification changes made under pressure, which is precisely the pattern that produces quality drift. A scheduled review protects both the price and the product.
Capacity reservation belongs in the same contractual frame. A buyer who commits to a seasonal volume should ask for a corresponding reservation of line time, because a commitment without a reservation is only a forecast - and forecasts are what get displaced when capacity tightens.
Where volumes justify it, an annual rolling forecast is better than per-order booking. It lets the production side plan material procurement and line loading, which is what actually shortens a window during peak season, and it gives the buyer a stronger claim on capacity when it matters.
Quality Control and Acceptance Standards
In OEM the buyer sets the acceptance standard, which is both the advantage of the model and its obligation. A buyer who does not set one inherits the producer's, and then has no basis for rejection.
Pre-shipment inspection to AQL 2.5 is the standard control and works well for this category. It defines sample size and acceptance numbers by lot size, it is understood on both sides, and it produces a documented result that can be referenced later if a dispute arises.
What AQL 2.5 does not do is define what counts as a defect. That is the buyer's job, and it should be written into the specification as a defect classification - critical, major and minor - with examples for each. A zipper that fails to close is critical; a cosmetic mark inside a lining pocket is minor. Without that classification, two parties inspect the same lot and reach different conclusions.
Attendance is the second discipline. Buyers and nominated agencies may attend inspection, and should whenever a new platform is released or a new channel partner is involved. Attendance converts a report into a conversation and resolves borderline calls in minutes rather than over email.
Independent verification supports the same objective. Reports issued by internationally recognised laboratories such as SGS give both sides a reference point that is not either party's opinion, which is precisely why they prevent arguments rather than merely settling them.
Finally, inspection should be tied to the packing list. Because the list is generated from the final inspection count rather than from an estimate, the discrepancy that most often starts a customs question never arises.
Capacity, Scheduling and Season Planning
OEM gives the buyer specification control but not capacity control, and capacity is what determines whether a programme lands on time during peak season.
Production capacity is booked, not assumed. A 35-50 day bulk window is a statement about the time the work takes, not about when a line is available, and during peak season the difference between the two can be several weeks. Booking against a confirmed sample approval date is what converts the window into a schedule.
Sampling is the scheduling lever with the most leverage. Samples take 6-10 working days, which is fast enough to run a comparison - a standard and a reinforced version, or two fabric options - and that comparison is the cheapest durability insurance available. It also means specification decisions should be complete before sampling starts rather than resolved during it.
Seasonality then compounds everything. Pet bag demand clusters around gifting periods and travel seasons, factory capacity tightens weeks before them, and freight availability tightens alongside. A programme that books late pays in both time and freight premium for exactly the service it could have secured cheaply earlier.
The reliable method is to work backwards from the shelf date: deduct clearance and distribution, deduct loading and inspection, deduct the bulk window, deduct sampling, and treat the remainder as the deadline for freezing specification and artwork. Programmes planned this way rarely miss a window; programmes planned forwards usually do.
Material lead time is the scheduling variable most often overlooked. A named fabric or hardware item may itself have a procurement window, and confirming it at specification stage prevents a situation in which the line is available but the input is not.
How OEM Differs From the Adjacent Models
OEM is best understood by contrast, because the boundaries between the three common models are frequently blurred in conversation and sharp in practice.
Against white label, the difference is specification ownership. White label inherits a platform and applies branding; OEM supplies the specification and builds to it. White label is faster and cheaper to start; OEM delivers more differentiation and better long-run margin. The crossover point is usually around 3,000 units a year.
Against original design, the difference is who fills the specification gap. In OEM the buyer supplies a complete tech pack; in an ODM arrangement the production base proposes or adapts the design and the buyer selects. ODM is faster to a finished product and carries less buyer-side design resource, at the cost of less differentiation.
In practice most programmes sit somewhere between. A buyer may supply a complete specification for the shell and hardware while relying on the production base for internal structure, which is a hybrid that works well provided both sides know which parts of the specification are theirs.
Choosing deliberately matters because each model has a different cost shape and a different control profile. A buyer who wants OEM but supplies an incomplete tech pack will receive ODM and be surprised by both the cost and the result.
Related guidance on original design manufacturing covers the adjacent model in detail, while brand programme strategy addresses how the choice serves a longer-term brand plan.
Buyers should state the model explicitly at enquiry. Naming whether a programme is OEM or ODM sets expectations about who produces the tech pack, and it prevents the common mismatch in which a buyer expects control they have not asked for and receives a design they did not choose.
Communication and Change Control in Contract Production
Contract production fails far more often through communication than through capability, and the failure mode is consistent: a decision was made, understood differently on each side, and discovered only when the goods arrived.
The first control is a single written channel with a named owner on each side. Technical questions, specification changes and approvals should travel through it rather than through parallel conversations, because parallel conversations produce parallel versions of the specification - and reconciliation happens at inspection, which is the worst possible time.
The second is a change-control rule with three elements: any change is written, any change produces a new specification version, and any change after sample approval is costed and scheduled before it is accepted. None of these is burdensome; together they remove the entire class of problems that arises from a verbal agreement made under time pressure.
The third is a defined approval gate. Sample approval should mean a specific thing - the sample is approved against version X of the specification, dated, with any deviations listed. An approval that means roughly that the sample looks right leaves no basis for rejecting a production lot that differs from it.
Tolerances deserve a specific mention because they generate more argument than any other element. Agreeing a tolerance band on every critical dimension at specification stage converts a subjective judgement into an objective check, and it is the single cheapest way to prevent a dispute at inspection.
Finally, agree what happens on disagreement. Naming a third-party reference - an independent laboratory result, a retained sample, a specified method - costs nothing at the outset and resolves in days an argument that would otherwise consume weeks of correspondence and, frequently, the relationship.
Programmes that run these controls hand off cleanly between seasons, absorb staff changes without losing specification knowledge, and scale without renegotiating first principles. Those are unglamorous advantages and they are worth more than any single commercial concession.
Retained samples deserve specific mention because they resolve disputes faster than any other mechanism. Keeping one approved sample per specification version, signed and dated, gives both sides a physical reference that predates the argument. It costs nothing to maintain and it ends discussions that would otherwise run for weeks.
The same reference should extend to the approved colour and finish standards. A signed shade reference and an approved hardware sample remove the two most subjective judgements in the category, and disagreements about both are otherwise resolved by opinion rather than by comparison.
Documentation retention periods should be agreed for the same reason. A claim arising two seasons after shipment can only be answered if the relevant records still exist, and agreeing how long they are kept - and in what form - is far easier at the start of a relationship than at the end of one.
Working Terms and What Leaves With the Goods
Production terms in a contract arrangement are standard and are designed to be auditable. MOQ is 500 pieces per colourway, mixed colourways are permitted within one order, and size splits inside a single style count toward the threshold - which is what allows a full size curve without multiplying the commitment.
Samples take 6-10 working days from a confirmed tech pack, which is the point at which the specification should already be complete. Bulk production takes 35-50 days after sample approval, and pre-shipment inspection runs to AQL 2.5 against the defect classification in the specification, with attendance permitted for buyers and nominated agencies.
The document set ships with the goods: bill of materials with named inputs, lot-referenced chemical and colour fastness reports, hardware declarations with cycle data, origin information, a packing list generated from the final inspection count, and photographs of every marking position. Reports can be issued in the buyer's name when requested at commissioning.
Terms are T/T 30/70 with shipment FOB Xiamen. Our SGS-verified production base operates to ISO 9001 quality management principles with BSCI social compliance auditing in place, which is what allows a buyer-supplied specification to hold across lots and seasons rather than drifting between them.
Where a buyer operates in a regulated destination, confirm at specification stage which documents must name them. A report or declaration issued to another party may not satisfy a channel requirement, and obtaining a corrected version after production is slower and sometimes impossible.
Agree a single point of contact for document requests. Chasing records through several channels is how a shipment loses a week, and one named owner on each side removes the delay entirely.
Order and quality terms
- MOQ 500 pieces per colourway; samples in 6-10 working days
- Bulk production 35-50 days after approval; AQL 2.5 inspection standard
- T/T 30/70 terms, FOB Xiamen, full document set per shipment
People Also Ask
How do we know whether our arrangement is genuinely OEM?
Test portability: could the same tech pack be handed to another competent production base and produce the same product? If not, design has been outsourced as well.
Why do tolerances matter so much?
Without them a dimension is a preference rather than a requirement. Dimensional drift across lots is the most common cause of a channel compliance failure.
What is the strongest clause for brand protection?
Brand-mark restriction on embossing and printing plates. It costs nothing to include and prevents your mark being used on another buyer's production.
Why should inspection be tied to the packing list?
Because a list generated from the final inspection count rather than an estimate removes the discrepancy that most often starts a customs question.
Should we run two specification options during sampling?
Yes. Sampling is fast enough to compare a standard and a reinforced version, and that comparison is the cheapest durability insurance available.
When should we move from white label to OEM?
Around 3,000 units a year, when competitors undercut a shared platform, or when channel ambition requires a specification story.
What is the most common hidden OEM cost?
Compliance and documentation, which are largely fixed and behave like tooling. At 500 units the allocation can exceed a dollar per piece.
Frequently Asked Questions
What does OEM mean for pet bag production?
You supply the design and specification and the production base builds to it. You control the specification and carry the development cost, without owning the underlying platform.
How is OEM different from white label?
White label inherits an existing platform and applies your branding. OEM builds to your specification, which takes longer to start but delivers more differentiation and better long-run margin.
How is OEM different from ODM?
In OEM the buyer supplies a complete tech pack. In ODM the production base proposes or adapts the design and the buyer selects, which is faster but less differentiated.
Who owns the tooling and patterns?
Whoever the agreement says. By default the producer holds them, so access on exit, exclusive use periods and pattern copies should be agreed before production.
How much does bespoke tooling cost?
Typically USD 300-2,500 per item depending on type: cutting dies, hardware moulds, embossing plates and printing screens each carry their own cost.
Should test reports be issued in our name?
Yes, and request it at commissioning. A report naming another party is weaker when a channel asks the brand to substantiate a claim, and reissue later may not be possible.
What must a pet bag tech pack contain?
Named materials and hardware, critical dimensions with tolerances, construction sequence, reinforcement locations, ventilation specification, labelling positions and performance targets.
What does AQL 2.5 not cover?
The definition of a defect. That is the buyer's job and should be written into the specification as a critical, major and minor classification with examples.
Can we attend pre-shipment inspection?
Yes. Buyers and nominated agencies may attend, which we recommend whenever a new platform is released or a new channel partner is involved.
How much development cost should we expect?
Typically USD 1,500-6,000 for a first season across tooling, patterns, sampling iterations and initial testing, amortised over units.
How long do samples and bulk production take?
Samples take 6-10 working days from a confirmed tech pack; bulk takes 35-50 days after sample approval, with pre-shipment inspection to AQL 2.5.
Do size splits count toward the minimum?
Yes. Size splits inside a single style count toward the colourway threshold, which makes a full size curve affordable at first order.
How should we plan around peak season?
Work backwards from the shelf date and book capacity against a confirmed sample approval date. The 35-50 day window describes the work, not line availability.
What payment and shipping terms apply?
T/T 30/70 with shipment FOB Xiamen. Tooling, exclusivity and report-issuance terms should be settled at quotation rather than after production.
Talk to QUANZHOU JUNYUAN BAGS about a wholesale pet bag order: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days under AQL 2.5 inspection.
Get a free quote Request a sample